Industry Insights
Anti-Static Plastic Pallets, Pallet Boxes, and Totes: Define the ESD Role
Separate the protected item, inner packaging, load-carrier role, and exact-model evidence before specifying an anti-static plastic pallet, pallet box, or tote.
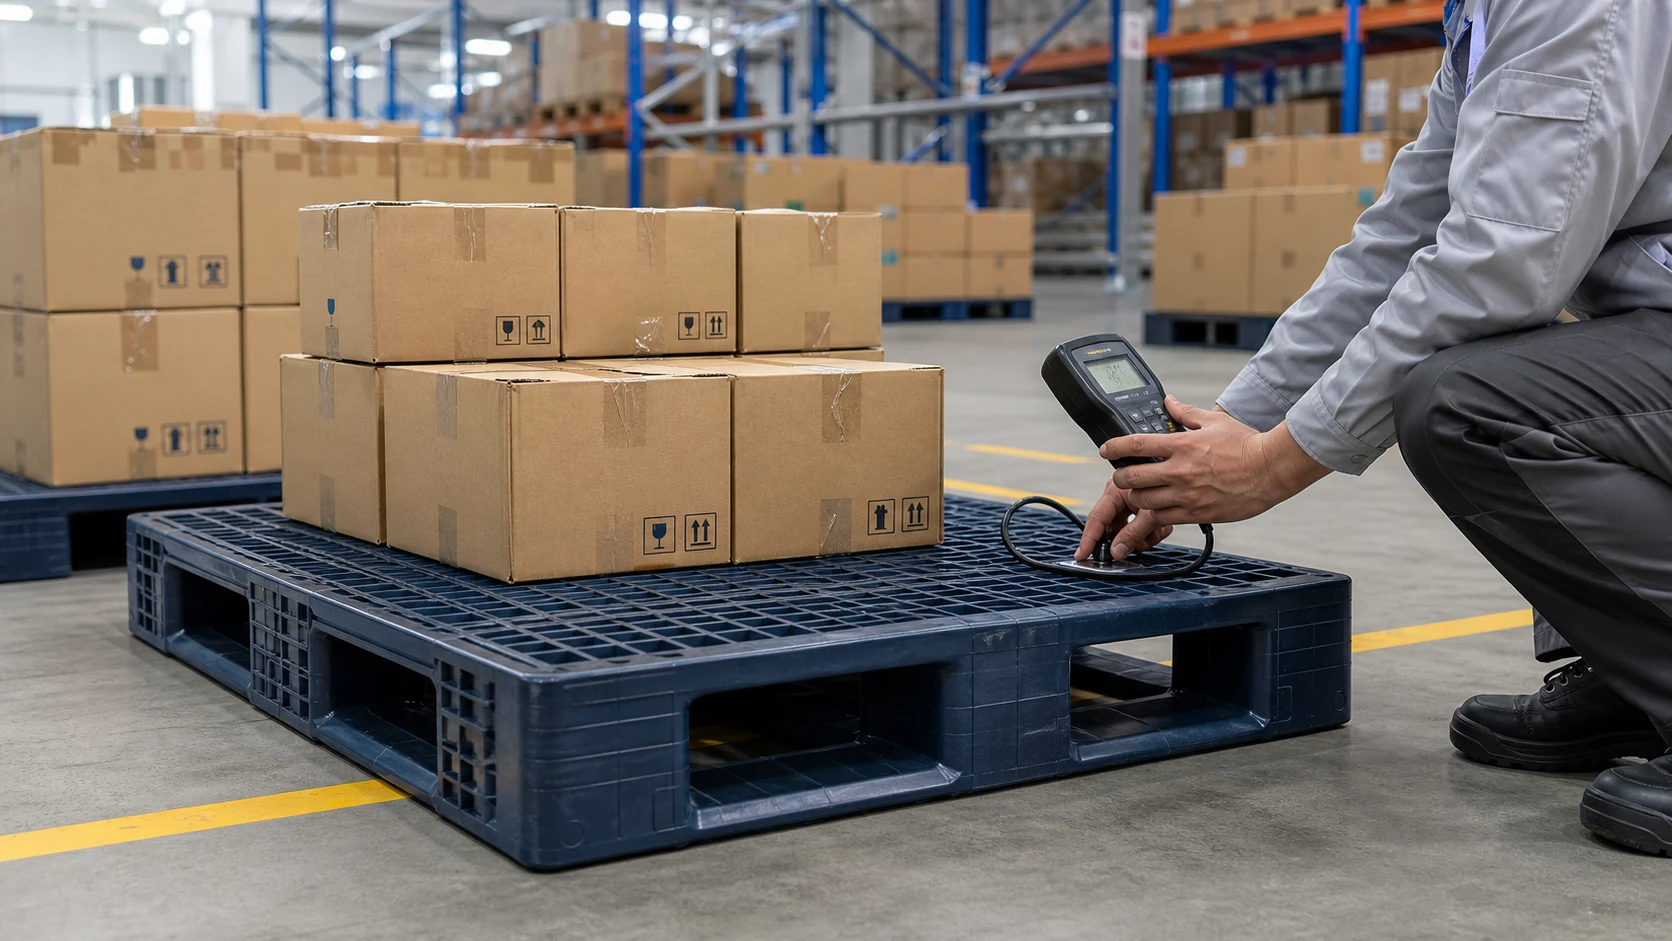
Anti-static plastic pallets, pallet boxes, and totes are often requested late in a sourcing project, after someone raises a concern about electronic parts, an ESD-controlled area, dry conditions, or a customer audit. The request sounds simple: “make the carrier anti-static.” In practice, that phrase does not identify what must be protected or what the carrier must do.
For electronic devices, static control belongs to the buyer’s complete ESD control program. The decision depends on the device sensitivity, inner packaging, where the carrier travels, whether packs are opened on it, the floor and grounding system, cleaning, wear, and the agreed test method. Ignition hazards involving flammable liquids, gases, powders, or electrically initiated devices require a separate safety review; they are not covered by the electronic-device scope used in this guide.
The useful sourcing question is:
What ESD role, if any, must the pallet, pallet box, or tote perform, and which exact-model evidence will prove it?
Start by separating product risk from warehouse preference
Not every warehouse needs ESD pallets. The first step is to identify what can actually be harmed by static charge.
Anti-static or static dissipative pallet requirements are usually worth evaluating when the load includes:
- electronic components, PCB assemblies, sensors, batteries, semiconductors, or precision instruments;
- packaging that is already controlled under an ESD program;
- powders, films, lightweight plastic parts, or materials that attract dust through static charge;
- liquids, aerosols, or chemical goods where the site safety team has identified ignition or discharge risk;
- customer-owned reusable pallets entering an ESD-controlled production or inspection area.
The requirement is weaker when the pallet only carries sealed commodity cartons through a normal warehouse with no ESD-sensitive products, no hazardous atmosphere, and no customer ESD specification. In that case, anti-static material may add cost without solving a real operational problem.
A good purchasing specification begins with the risk case, not the product name. Instead of writing “anti-static pallet required,” define why the pallet needs static control and where it will be used.
Know the difference between anti-static, dissipative, and conductive
These terms are often used as if they mean the same thing. They do not.
| Term used in sourcing | Practical meaning | Common buying risk |
|---|---|---|
| Anti-static | Reduces charge generation or static build-up | May not provide a controlled path to ground |
| Static dissipative | Allows charge to decay in a controlled way when connected to the right system | Needs measurable resistance range and test method |
| Conductive | Provides a lower-resistance path for charge movement | Can be inappropriate if the site is not designed for conductive handling |
| Standard plastic | Usually insulating unless modified or treated | Can hold charge in dry or high-friction conditions |
For B2B procurement, the safest wording is usually not a broad label. It is a measurable requirement: surface resistance range, test method, test locations, conditioning environment, and acceptance rule.
Color should never be treated as proof. A black pallet is not automatically conductive. A blue pallet is not automatically safe for ESD areas. Additives, compound formulation, molding consistency, surface wear, and contamination all affect performance.
Map every interface where static can be created
Static charge is generated by contact and separation. In warehouses, that can happen at more points than buyers expect.
Review the full handling route:
- pallet sliding on a plastic or coated floor;
- cartons moving against the pallet deck;
- stretch film, strapping, or plastic liners contacting the load;
- forklift forks entering and leaving pallet openings;
- conveyor rollers, chain transfers, turntables, and lift tables;
- operators removing trays, bags, or ESD packaging from the pallet;
- dry storage rooms, air-conditioned production zones, or winter shipping lanes.
This is especially important in automated flow. A pallet may have acceptable static behavior in slow forklift movement but behave differently on conveyors where repeated contact points, faster transfer, and sensor positions create new failure modes. If the same pallet will run through conveyors or AS/RS equipment, combine ESD requirements with the normal automation checks covered in the automation-ready plastic pallet specification .
The goal is not to make the pallet responsible for the whole ESD system. The goal is to ensure the pallet does not become the uncontrolled weak point inside that system.
Treat chemical and flammable areas as a safety review, not a catalog choice
Chemical handling creates two separate questions: containment and static risk.
A spill-control pallet can help contain leaked liquids and separate drums from the floor. For example, a product such as the 130130 spill containment pallet is relevant when the problem is secondary containment for drums or industrial liquid storage. That does not automatically make it an ESD-safe pallet.
If the site handles flammable liquids, solvent vapors, combustible dust, aerosols, or hazardous-area materials, the pallet decision should be reviewed by the buyer’s EHS or safety team. The chemical and spill-control handling page is a useful starting point for containment and chemical contact questions, but static control must be defined separately.
For these applications, do not rely on supplier statements such as “anti-static available” without site-specific approval. Confirm:
- whether static control is required by the facility’s risk assessment;
- whether grounding or bonding is needed during storage or transfer;
- whether the pallet material, floor, racks, and equipment create a complete discharge path;
- whether cleaning chemicals or liquid residue will change surface behavior;
- whether the pallet will enter classified or restricted zones.
In chemical areas, the wrong pallet is not only a performance issue. It can become a safety-control gap.
Decide whether the pallet itself must be ESD controlled
Sometimes the load is ESD-sensitive, but the pallet does not need to be the primary control layer. The answer depends on where the pallet sits in the process.
An ESD-controlled pallet is more likely to matter when:
- components are placed directly on the pallet or on conductive trays carried by the pallet;
- operators open cartons or remove ESD bags while goods remain on the pallet;
- pallets enter production, inspection, kitting, or clean assembly zones;
- pallets stay inside an ESD-protected area for long dwell times;
- customer procedures require all load carriers in the area to meet a defined resistance range.
The pallet may be less critical when:
- goods remain sealed inside approved ESD packaging;
- the pallet stops at the receiving dock and never enters the ESD zone;
- cartons are transferred to approved carts or shelves before opening;
- the customer’s ESD program controls the item-level packaging rather than the shipping pallet.
This distinction prevents over-specification. It also protects the buyer from under-specification when pallets quietly cross from general warehouse space into controlled production areas.
For a pallet box or tote, separate four layers
A pallet box or tote can contain ESD-sensitive devices without automatically being the protective packaging. IEC 61340-5-1:2024 places packaging, transport, and handling inside an ESD control program. IEC 61340-5-3:2022 addresses properties and classification for packaging intended to protect ESD-sensitive devices. Neither reference approves a supplier’s exact carrier or makes every outer container perform the same function as an inner ESD bag, tray, or cushioning system.
Write the requirement in four layers:
- Protected item. Identify the component, assembly, or equipment and the sensitivity or customer program that controls it. A generic statement such as “electronics” is not an acceptance limit.
- Inner packaging. State whether devices remain sealed in qualified bags, trays, dividers, or other protective packaging, and where that packaging is opened. Do not assume a dissipative outer box compensates for an unsuitable inner pack.
- Carrier role. Decide whether the pallet box or tote stays outside the ESD-protected area, crosses into it while sealed, supports unpacking, contacts unpackaged items, or must connect to a defined grounding system. The required property follows this role.
- Finished-carrier evidence. Name the test method, conditioning, measurement locations, limits, sample plan, and retest trigger. Include the base, walls, lid, hinges, latches, dividers, contact points, cleaning, abrasion, repairs, and material or process changes when they can affect the result.
If qualified inner packs remain sealed and the outer carrier never enters the controlled area, a standard pallet box may be acceptable—but the buyer’s program must make that decision. If the carrier enters the area, supports opening, or directly contacts sensitive items, the buyer should define its function and verification method before asking for a model. The supplier should then state which exact finished-carrier records are available. If those records do not exist, do not replace them with a colour, resin name, additive label, or broad claim of ESD compliance.
Specify performance after real use, not only at shipment
Some anti-static properties depend on additives, surface condition, and environment. A pallet may pass a basic test when new and fail after abrasion, washing, outdoor exposure, dust build-up, or repeated forklift contact.
For reusable pallets, ask how performance is maintained through the expected life cycle:
- Is the anti-static property built into the material compound or applied as a surface treatment?
- Does washing, detergent, disinfectant, or chemical residue affect resistance?
- Are there temperature or humidity conditions where performance changes?
- Which pallet zones should be tested after wear: deck, runners, corners, fork-entry areas?
- What is the retest frequency for pallets used in controlled areas?
If the pallet will be cleaned regularly, include the cleaning method in the test plan. Food, pharmaceutical, electronics, and chemical sites often use very different cleaning agents, and those agents can change the surface condition that static control depends on.
Write a clear RFQ requirement
An RFQ should translate the risk into testable supplier obligations. A useful anti-static pallet clause may include:
- application: product type, packaging type, and whether pallets enter an ESD-controlled zone;
- required static behavior: anti-static, dissipative, or conductive as defined by the buyer’s program;
- measurement: surface resistance or other required test, including equipment and method;
- test locations: top deck, bottom runners, side surfaces, and any contact zones;
- environmental conditioning: humidity, temperature, and whether samples are tested before or after cleaning;
- sample size: number of pallets per lot or per shipment to verify;
- documentation: test report, material declaration, lot traceability, and change-control rule;
- rejection criteria: what happens if results drift outside the agreed range.
This can sit inside a broader purchasing document. If the buyer is already preparing a technical request, the plastic pallet RFQ specification checklist can be extended with a dedicated ESD section.
Avoid short clauses such as:
Pallet must be anti-static.
Use a more complete version:
Pallet material and finished pallet surface must meet the static-control requirement defined by the buyer’s ESD program. Supplier must provide test results for agreed pallet zones under agreed conditioning conditions. Performance must remain within the approved range after normal cleaning and handling during the sample trial.
The second clause gives procurement, quality, and the supplier something measurable to approve.
Validate with the actual handling route
Sample validation should not stop at a bench reading. Use the pallet in the real process.
A practical trial can include:
- Measure sample pallets before use and record the method.
- Build the normal unit load with actual cartons, trays, bags, or containers.
- Move the pallet through receiving, staging, production entry, storage, and dispatch.
- Include the normal floor, forklift, conveyor, rack, or pallet-jack interfaces.
- Test again after the handling cycle and after cleaning if cleaning is part of the process.
- Check whether labels, stretch film, liners, or protective sheets change the static-control result.
- Record any handling damage, surface abrasion, or contamination that affects test points.
For incoming control, the inspection plan should identify which pallets are sampled and how records are kept. The same logic used in a plastic pallet incoming inspection plan can be adapted for ESD-related acceptance checks.
Watch common failure points
Several mistakes repeat across anti-static pallet projects.
Relying on color. Color is a visual cue, not a technical result.
Ignoring the load packaging. A dissipative pallet does not fix insulating stretch film or non-compliant trays.
Testing only one surface. The deck, runner, and contact edges may perform differently.
Forgetting humidity. Dry rooms and winter lanes can increase static problems.
Assuming metal reinforcement solves static. Steel tubes may improve stiffness, but they do not automatically control surface charge on plastic contact areas.
No change-control rule. A small material or additive change can alter ESD behavior even when dimensions and load ratings remain the same.
Approving samples without lot checks. ESD performance must be consistent enough for production supply, not just one demonstration pallet.
These risks are manageable when they are written into the specification before ordering.
Practical decision rule
Choose an anti-static pallet, pallet box, or tote only when the handling route and the buyer’s ESD program give it a defined control function, then express that function in measurable terms.
Start with the protected item and inner packaging. Confirm whether the carrier enters an ESD-protected area, supports opening, or touches unpackaged devices. Separate containment from ESD protection and separate electronic-device protection from ignition-hazard review. Define the required behavior, test method, carrier zones, environmental conditions, and retest rules. Validate the exact finished model through the real route before bulk purchase.
The right ESD load carrier is not a product with a special label. It is an exact finished model whose documented static behavior, structure, cleaning tolerance, and inspection plan fit the buyer’s complete control system.